From pouring to track installation, all under one roof.
Hadfield manganese steel poured at our plant, with mold-fill simulation before casting.
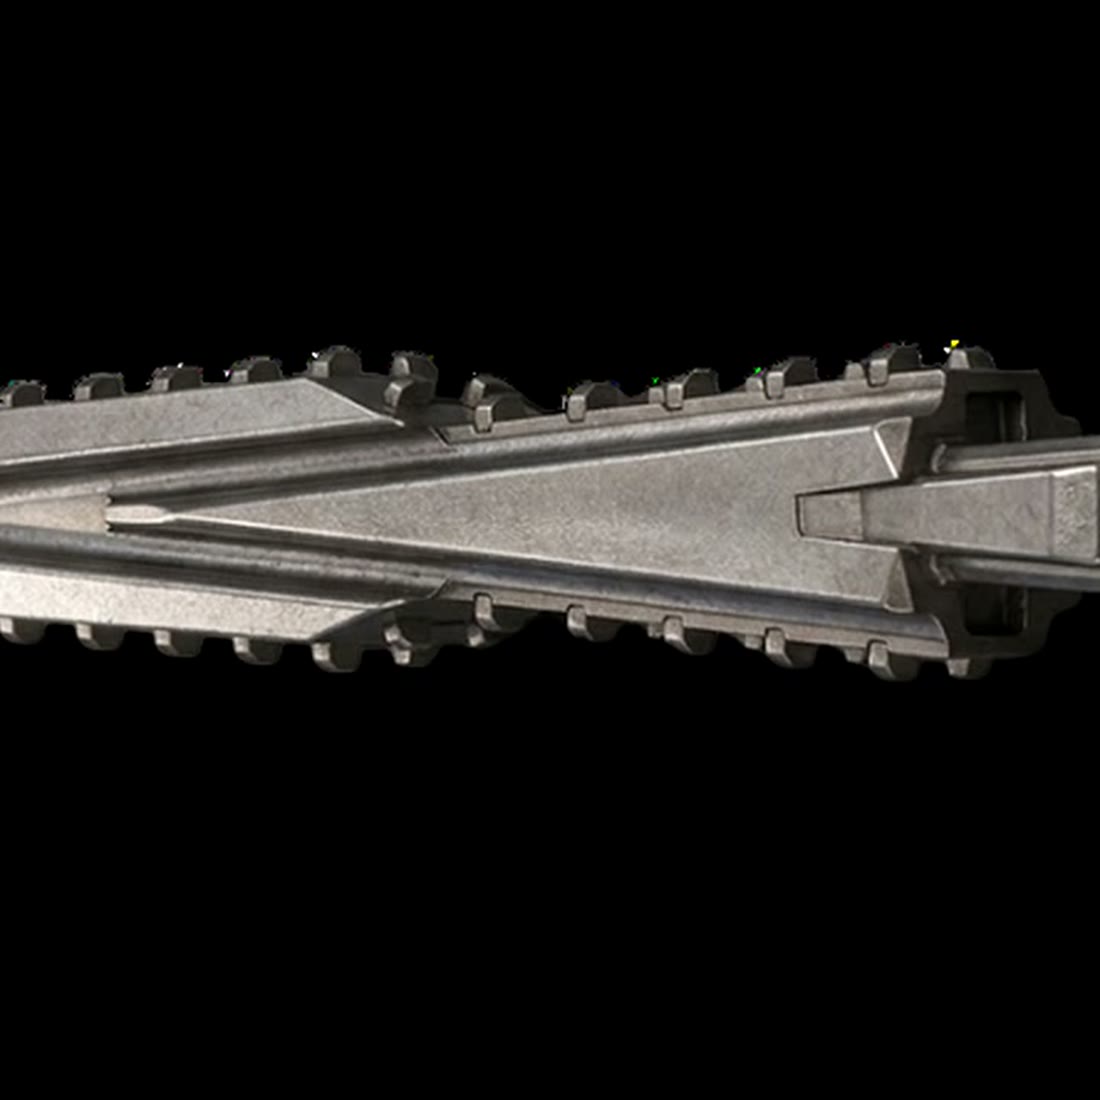
The only one in Latin America: the insert is shock-wave hardened per ASTM A128, ≥ 352 HB to a depth of ≥ 20 mm.
Rails, tie plates and clips are bench-assembled against the drawing; the set is counted and documented.
Every piece is hand-detailed in the shop before it goes to inspection.
Dimensional, hardness and visual: every set is measured before shipping.
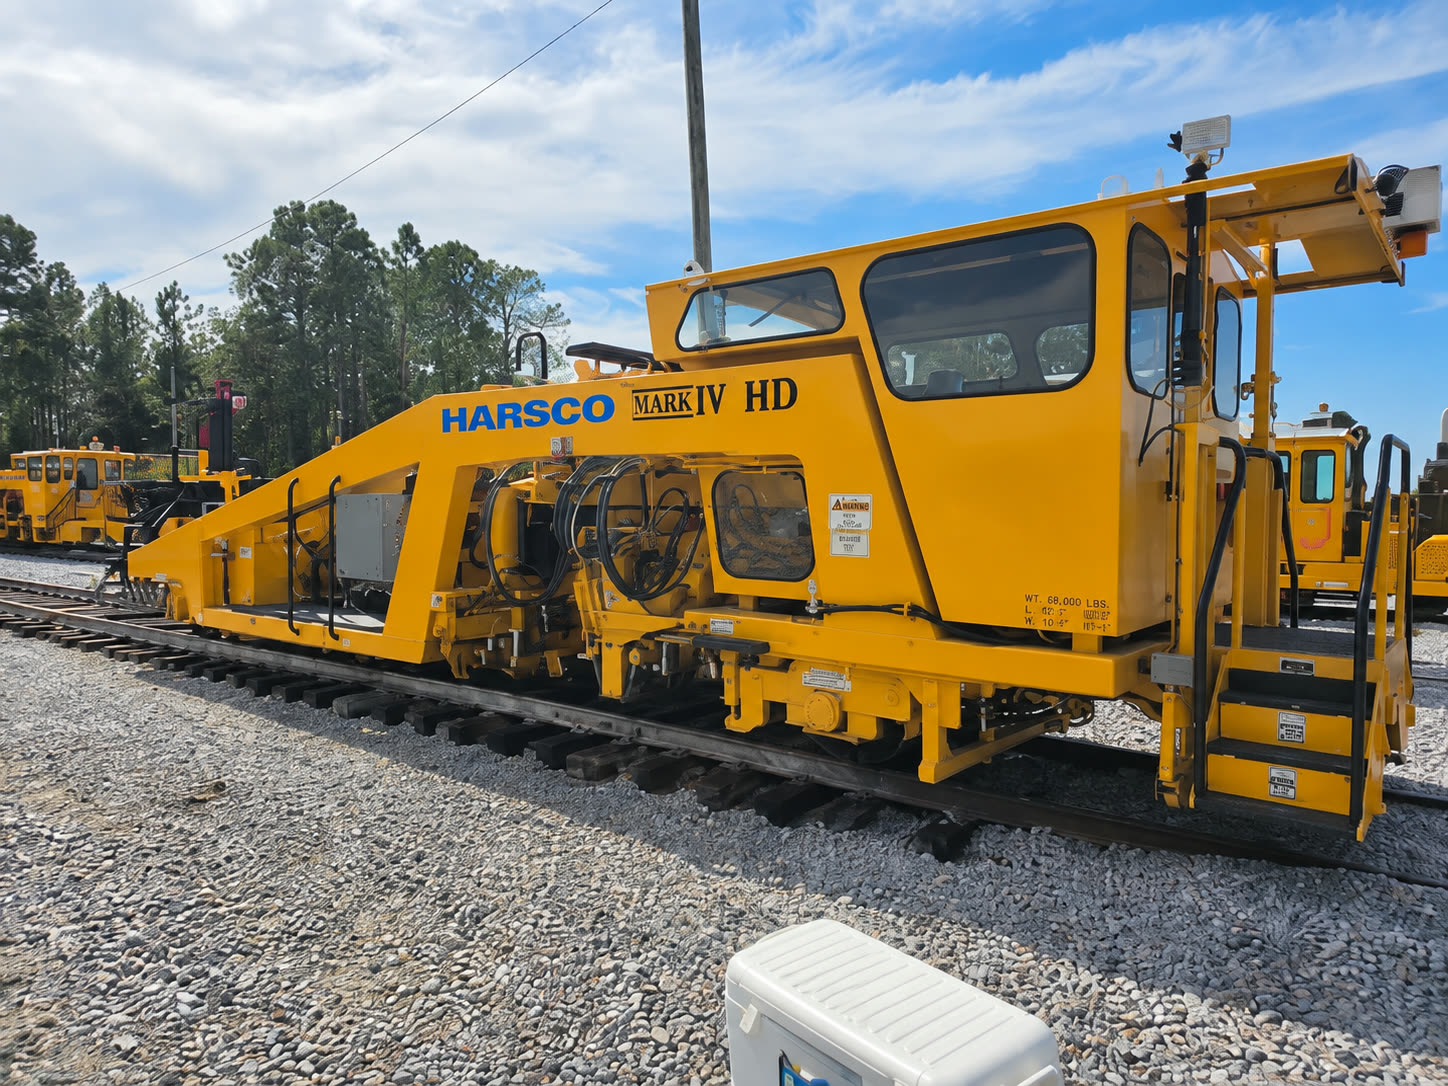
Track installation with our own hi-rail equipment: assembly, alignment, leveling and geometry adjustment.
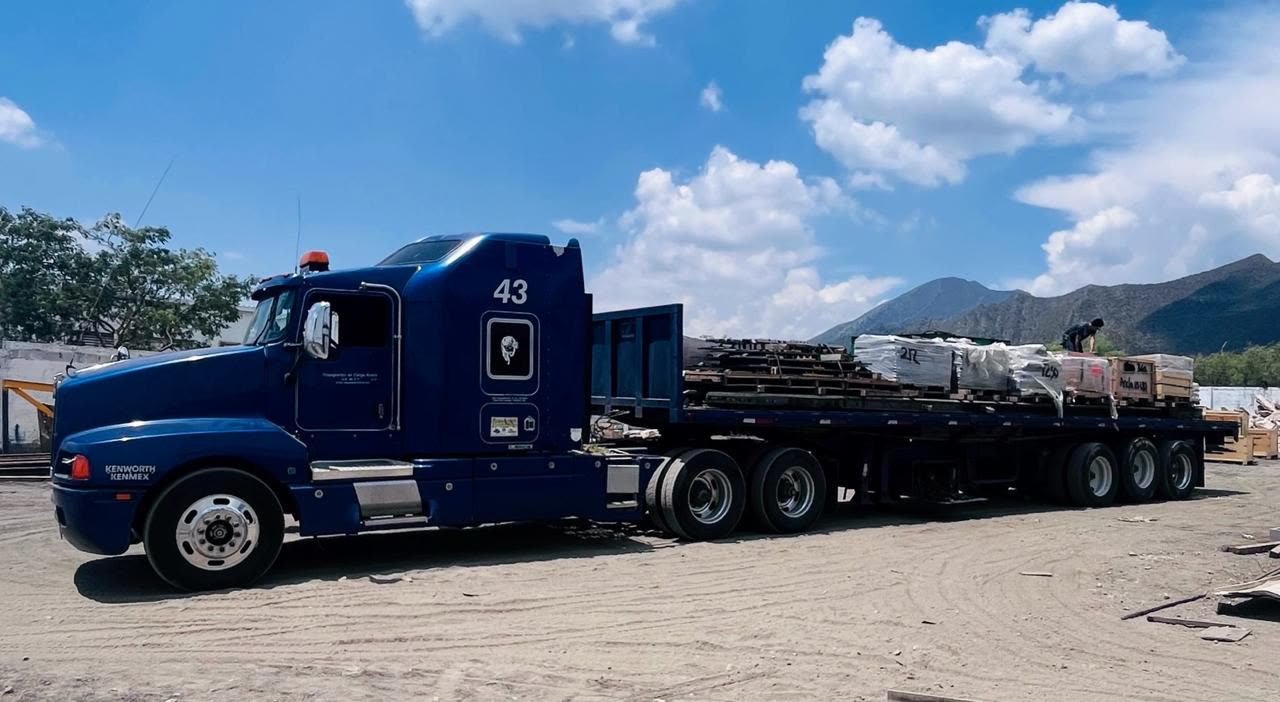
The turnout leaves the plant assembled on our flatbeds and arrives complete at the job site.
Hadfield manganese steel poured into the mold, cooled under control and inspected against its own drawing before the final treatment.
Hadfield steel comes out of the foundry austenitic and relatively soft. The shock wave transforms it: it deforms the crystal lattice at depth, compacts it and hardens it — without making it brittle and without altering the drawing geometry.
See how explosive hardening works →